What Causes Deformation in Industrial Steel Balls?
Although steel balls have a relatively simple geometric shape, manufacturing high-quality industrial steel balls requires precise control at every stage.
A typical production process may include:
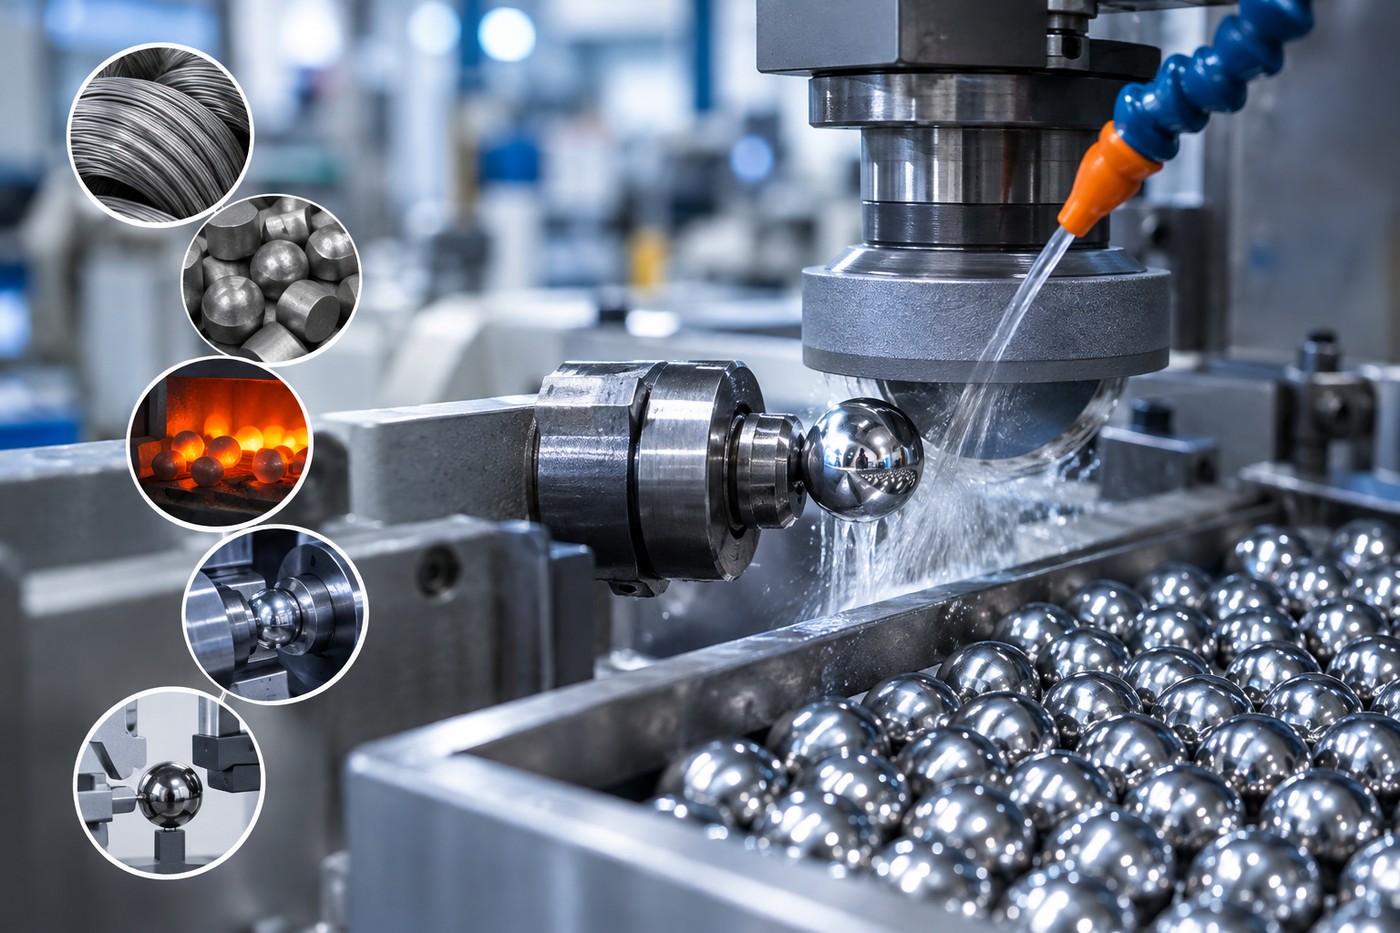
Raw Material → Cold Heading/Forming → Flash Removal → Soft Grinding → Heat Treatment → Hard Grinding → Fine Grinding → Lapping/Polishing → Inspection → Packaging
Each process can influence the final dimensional accuracy and roundness of the steel ball.
The main causes of deformation include:
- Internal stresses in the raw material
- Inconsistent ball blank dimensions
- Tool or die wear
- Uneven forming pressure
- Improper heat treatment
- Excessive grinding pressure
- Insufficient cooling during grinding
- Uneven material removal
- Equipment instability
- Inadequate quality inspection
For precision steel balls, controlling these factors is essential for achieving stable production results.
1. Start With Stable Raw Materials
Raw material quality is the foundation of industrial steel ball manufacturing.
Steel wire and other raw materials can contain residual stresses generated during rolling, drawing, cutting, or other upstream processes. If these stresses are not properly controlled, they may be released during forming, grinding, or heat treatment.
This can result in dimensional changes or roundness variation.
For this reason, professional steel ball manufacturers should carefully control:
- Material grade
- Chemical composition
- Raw material dimensional tolerance
- Material cleanliness
- Internal structure
- Surface condition
- Batch consistency
For applications such as bearings and precision machinery, stable raw material quality helps reduce dimensional variation throughout subsequent processes.
2. Control the Cold Heading and Forming Process
Cold heading is commonly used to manufacture small and medium-sized steel ball blanks.
During this process, steel wire is cut to a specific length and formed into a ball-shaped blank using precision dies.
If the forming process is not properly controlled, several problems may occur:
- Uneven ball blank dimensions
- Irregular material distribution
- Excessive flash
- Off-center forming
- Increased machining allowance
- Inconsistent ball geometry
Important factors include:
Die Accuracy
Worn or improperly designed dies can affect the geometry of the ball blank.
Cutting Length
Inconsistent wire cutting can result in different material volumes entering the forming process.
Forming Pressure
Stable forming pressure helps maintain consistent ball blank dimensions.
Equipment Alignment
Proper alignment between the forming tools and equipment is important for maintaining dimensional consistency.
Controlling these parameters at the beginning of production reduces the amount of correction required during later grinding processes.
3. Maintain Proper Machining Allowance
One common mistake in steel ball manufacturing is assuming that a larger machining allowance provides more room for correction.
In reality, excessive machining allowance can increase production time, grinding load, heat generation, and dimensional variation.
A better approach is to establish an appropriate machining allowance based on:
- Final ball diameter
- Required precision grade
- Material type
- Heat treatment requirements
- Grinding process
- Surface finish requirements
The goal is to provide sufficient material for correction while avoiding unnecessary material removal.
A stable production process should follow the principle:
Accurate forming → controlled heat treatment → controlled grinding → precision finishing
This helps reduce the risk of deformation during later processes.
4. Control Grinding Pressure
Grinding is one of the most important processes in precision steel ball manufacturing.
After heat treatment, hard grinding is commonly used to remove unwanted material, correct dimensional deviations, and improve roundness.
However, excessive grinding pressure can create several problems.
A typical chain of events may be:
Excessive Grinding Pressure → Increased Friction → Heat Generation → Thermal Stress → Dimensional Instability
Therefore, manufacturers need to carefully control:
- Grinding pressure
- Grinding speed
- Feed rate
- Material removal rate
- Grinding time
- Abrasive condition
- Cooling performance
For precision steel balls, it is generally preferable to use controlled, progressive material removal rather than attempting to achieve the final dimension through aggressive grinding.
5. Prevent Thermal Deformation During Grinding
Heat generated during grinding can affect steel ball dimensions.
When a steel ball becomes locally heated during machining, thermal expansion can temporarily change its dimensions. After cooling, the dimensions may change again.
This is particularly important when manufacturing high-precision steel balls.
Effective cooling helps control the temperature of the grinding zone and reduce thermal effects.
Important cooling parameters include:
Coolant Flow
The coolant should effectively reach the grinding contact area.
Coolant Temperature
Stable coolant temperature helps maintain consistent processing conditions.
Coolant Cleanliness
Proper filtration reduces the impact of grinding debris on the machining process.
Cooling Position
The coolant should be properly directed toward the contact area between the steel ball and grinding surface.
Effective thermal management contributes to better dimensional stability and surface quality.
6. Optimize Heat Treatment to Minimize Dimensional Changes
Heat treatment is a critical stage in steel ball manufacturing.
Bearing steel balls and other high-performance steel balls are commonly heat treated to achieve the required combination of:
- Hardness
- Wear resistance
- Strength
- Fatigue resistance
- Dimensional stability
However, heating, soaking, quenching, and tempering can also cause dimensional changes.
During heat treatment, steel undergoes thermal expansion, cooling contraction, and microstructural transformation.
Therefore, manufacturers need to control:
- Heating temperature
- Soaking time
- Furnace temperature uniformity
- Loading conditions
- Quenching conditions
- Tempering parameters
- Cooling rate
Different steel grades and ball diameters require different heat treatment parameters. A standardized process should therefore be adapted to the material and application requirements.
7. Improve Dimensional Stability After Heat Treatment
For high-carbon chromium bearing steels and similar materials, the microstructure after heat treatment can influence long-term dimensional stability.
Residual austenite, for example, can contribute to dimensional changes when microstructural transformations occur over time.
For high-precision applications, manufacturers may use carefully controlled heat treatment and, where appropriate, additional processes designed to improve dimensional stability.
This is particularly relevant for:
- Precision bearing steel balls
- High-speed bearing balls
- Automotive bearing balls
- Precision mechanical components
- High-speed rotating equipment
The exact process should be determined according to the steel grade, ball diameter, required hardness, dimensional tolerance, and application conditions.
8. Control Grinding Tool Wear
Grinding tools and finishing equipment gradually wear during continuous production.
If tool wear is not properly monitored, it can result in:
- Dimensional variation
- Roundness deviation
- Uneven material removal
- Changes in surface roughness
- Increased batch-to-batch variation
Professional steel ball manufacturers should establish appropriate inspection, adjustment, and replacement procedures for grinding tools.
This is especially important for large-volume B2B production, where even a small process deviation can affect a significant number of steel balls.
9. Maintain Batch-to-Batch Consistency
Industrial customers typically purchase steel balls in large quantities rather than as individual pieces.
Therefore, quality control should focus not only on whether one steel ball meets the specification, but also on whether the entire batch maintains consistent performance.
Important parameters include:
- Ball diameter
- Diameter variation
- Roundness
- Surface roughness
- Hardness
- Material consistency
- Dimensional stability
- Surface condition
Consistent manufacturing processes help minimize variations between individual balls and production batches.
This is particularly important for bearing applications, where differences between rolling elements can affect the operating performance of the entire bearing assembly.
10. Use Proper Inspection and Quality Control
Preventing deformation requires more than process experience. Reliable inspection equipment and quality control procedures are essential.
Common inspection items for industrial steel balls include:
Ball Diameter
Measures the actual ball diameter and dimensional variation.
Roundness
Determines how closely the steel ball approaches an ideal spherical shape.
Surface Roughness
Evaluates the quality of the finished ball surface.
Hardness
Verifies whether the heat-treated steel ball meets the required hardness specification.
Visual Inspection
Checks for defects such as:
- Cracks
- Scratches
- Dents
- Pits
- Grinding burns
- Surface defects
- Corrosion
Dimensional Grading
For precision steel balls, dimensional grading can help group balls according to their size and improve consistency for specific applications.
Key Factors for Preventing Steel Ball Deformation
Preventing deformation is not the responsibility of one individual process. It requires coordinated control throughout the entire manufacturing workflow.
| Manufacturing Stage | Potential Risk | Key Control |
|---|---|---|
| Raw Material | Internal stress and material variation | Material and batch control |
| Wire Preparation | Dimensional variation | Wire diameter and cutting accuracy |
| Cold Heading | Irregular ball blanks | Die accuracy and forming pressure |
| Flash Removal | Uneven surface | Equipment condition and machining control |
| Soft Grinding | Dimensional variation | Controlled machining allowance |
| Heat Treatment | Thermal and structural changes | Temperature and cooling control |
| Hard Grinding | Heat generation and roundness variation | Grinding pressure and cooling |
| Fine Grinding | Uneven material removal | Small and controlled machining allowance |
| Lapping | Precision variation | Pressure and processing time |
| Final Inspection | Defective products | Diameter, roundness, hardness and surface inspection |
Why Process Control Matters for Industrial Steel Ball Manufacturing
For B2B buyers, selecting an industrial steel ball supplier should involve more than comparing material and price.
The performance of a steel ball depends on the complete manufacturing process.
From raw material preparation to forming, grinding, heat treatment, finishing, and inspection, every stage can influence the final product.
A professional steel ball manufacturer should therefore have the capability to control the entire production chain.
Depending on the application, manufacturers may supply:
- Stainless Steel Balls
- Carbon Steel Balls
- Bearing Steel Balls
- Chrome Steel Balls
- Precision Steel Balls
- Industrial Steel Balls
- Custom Steel Balls
Customized solutions can be developed according to the customer's requirements for diameter, material, hardness, precision grade, surface finish, operating environment, and application.
Why Choose Huarui Steel Ball?
Changzhou Huarui Steel Ball Co., Ltd. focuses on the manufacturing and supply of industrial steel balls for B2B customers.
We emphasize process control throughout the manufacturing chain, from raw material selection and ball forming to heat treatment, grinding, finishing, and final inspection.
Our goal is not simply to produce steel balls that meet a dimensional specification, but to provide stable quality, consistent dimensions, reliable roundness, controlled surface finish, and batch-to-batch consistency for industrial applications.
Whether you need bearing steel balls, carbon steel balls, stainless steel balls, chrome steel balls, or customized steel balls, we can develop the appropriate manufacturing solution according to your technical requirements.